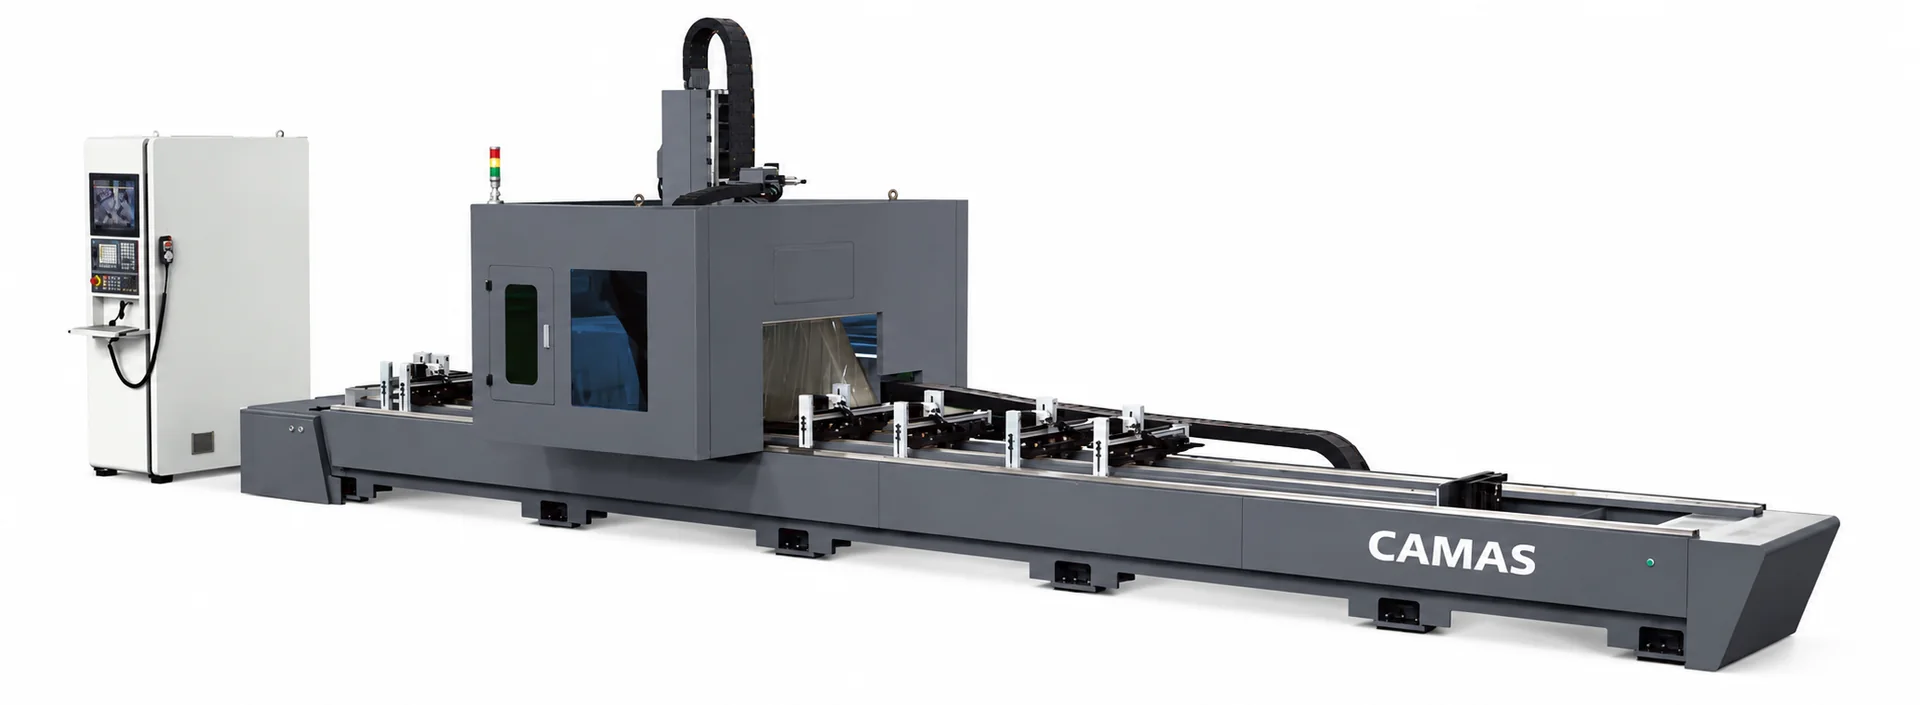
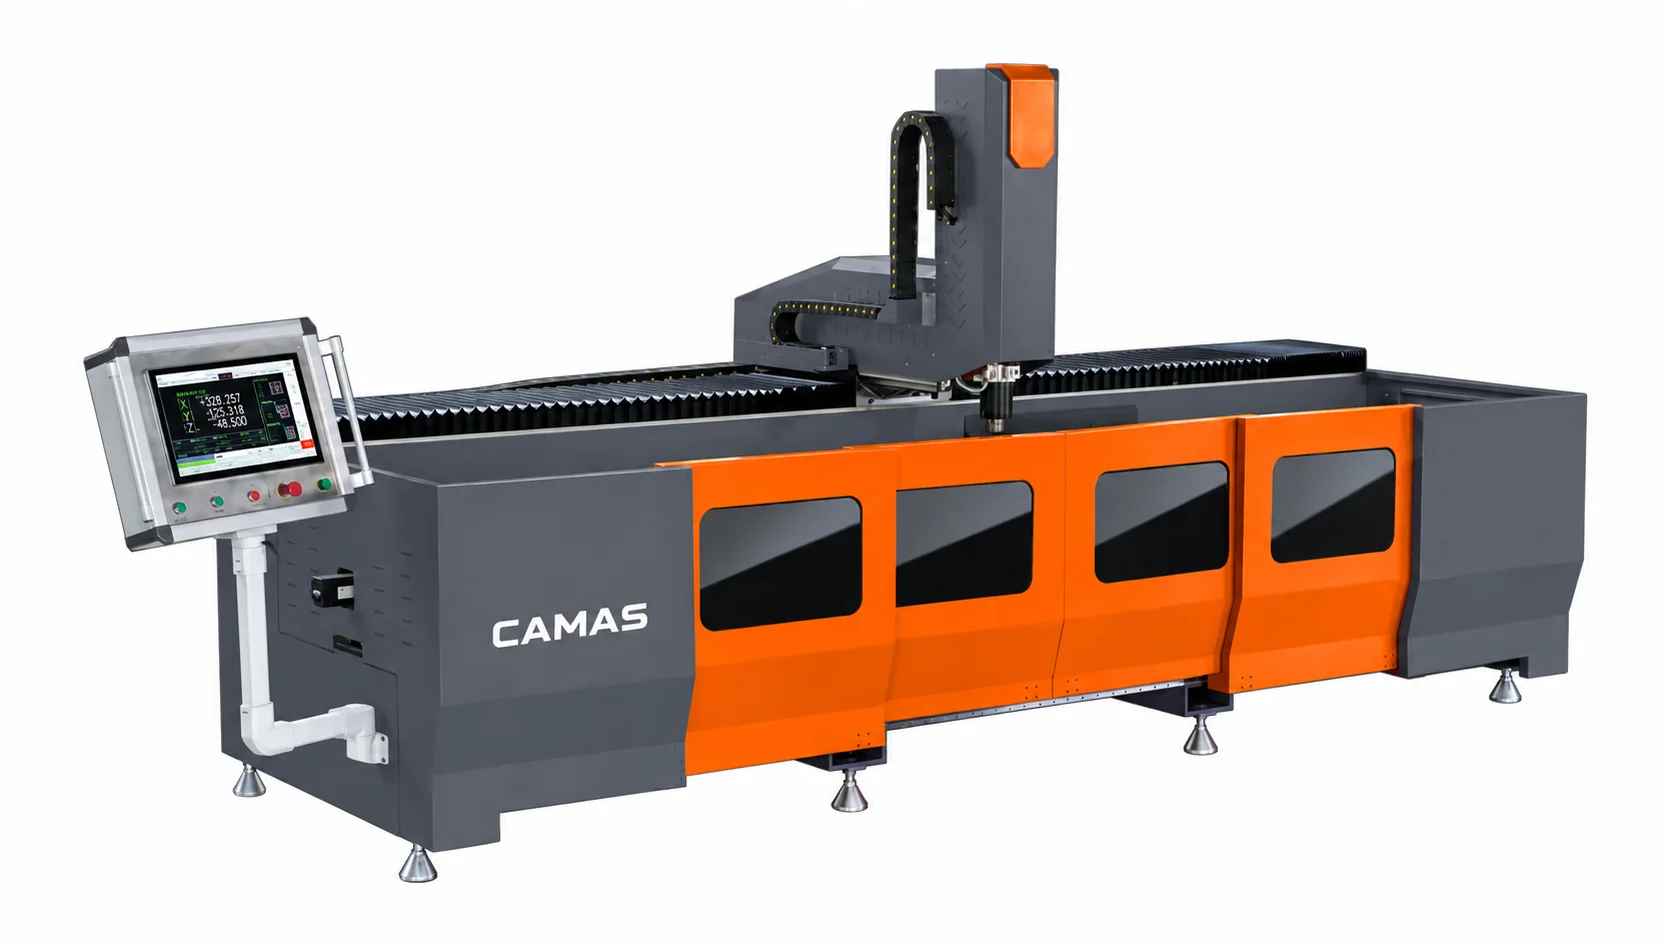
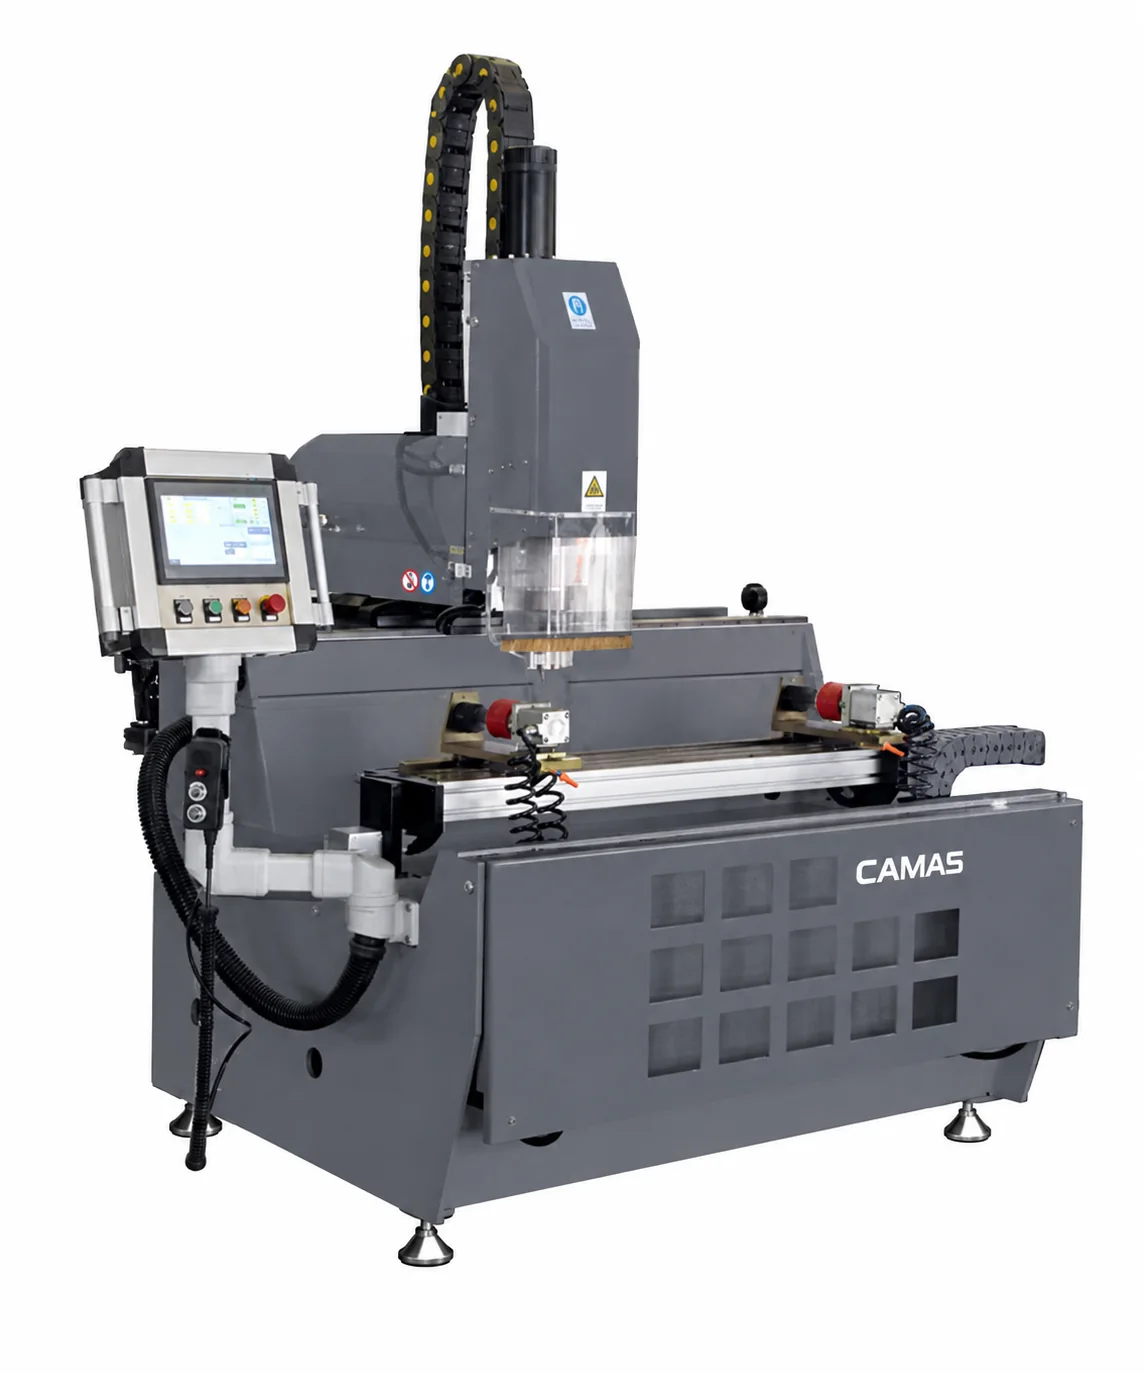
Final configuration and tooling are matched to your application.
01 / THE APPLICATION
Three-face features with a rotating worktable
Drill, mill, chamfer and engrave profile features with one clamping setup.
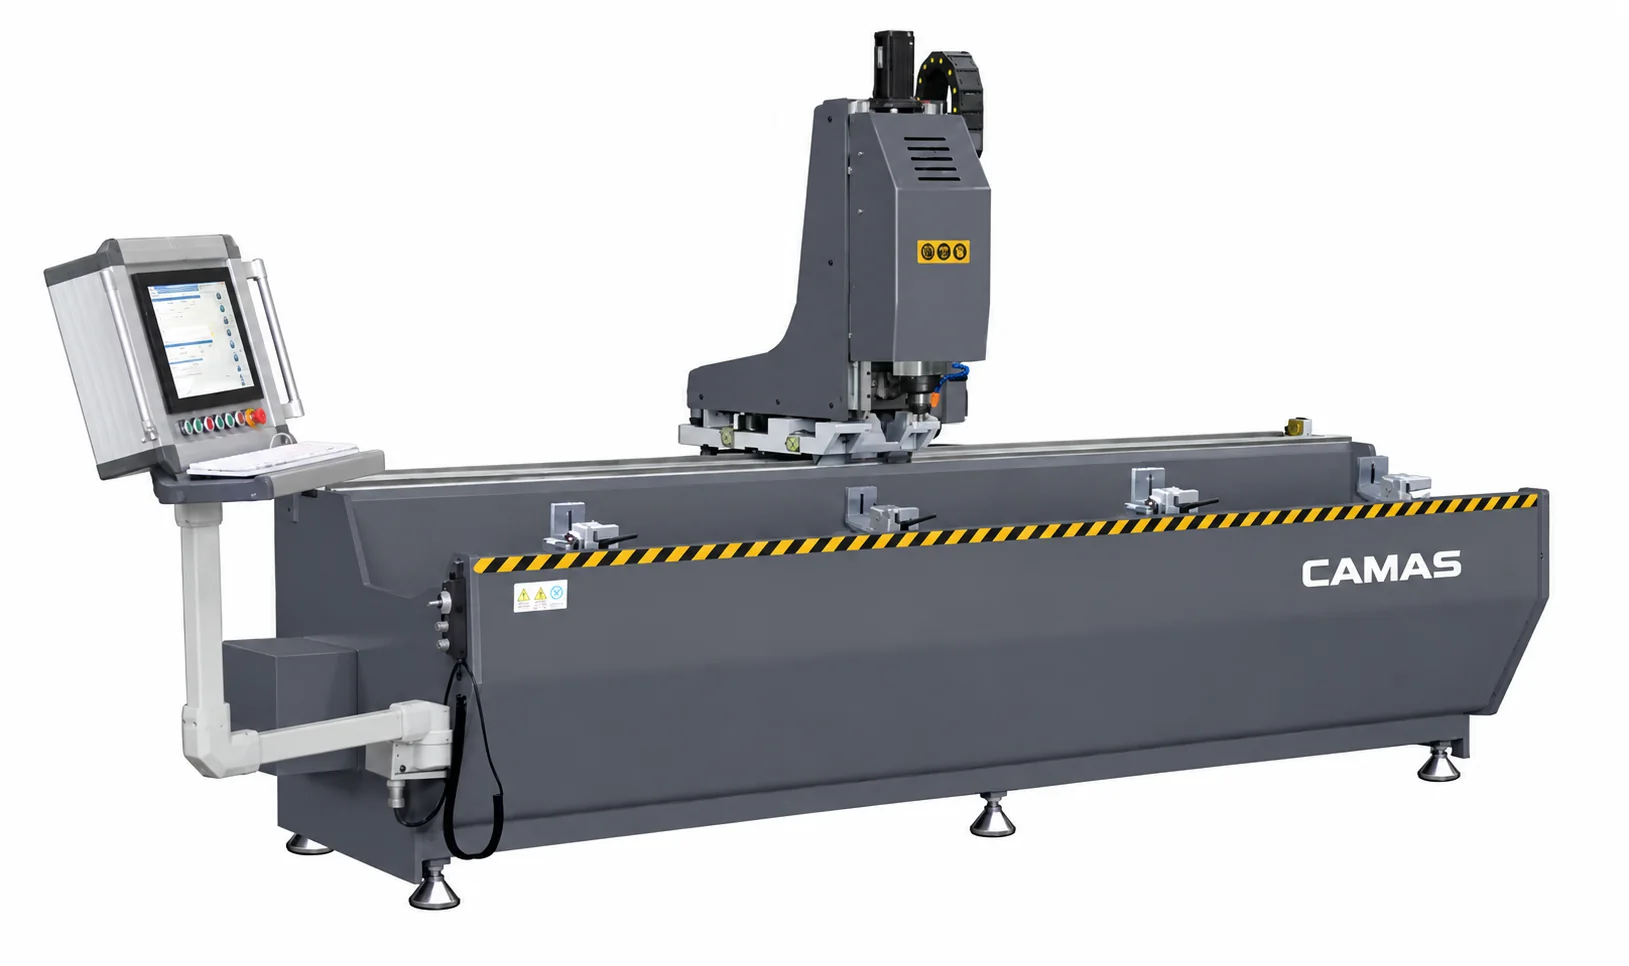
The published worktable positions are −90° / 0° / +90° (three faces, one clamping). Match the hole and slot locations on each face to the table positions, clamp layout and cutter access; the axis travels still need to be checked against the complete part.
CNC machining
Three-face machining
Application-led configuration
Define your tools and working requirements from the component drawing.
02 / TECHNICAL OVERVIEW
LZX-CNC-3200 specifications
CAMAS LZX-CNC-3200 technical specifications
Equipment line
Aluminum Profile Machinery
Model
CAMAS LZX-CNC-3200
Axes
3
X-axis travel
3,150 mm
Y-axis travel
330 mm
Z-axis travel
280 mm
Worktable positions
−90° / 0° / +90° (three faces, one clamping)
Spindle power
5.5 kW
Maximum spindle speed
18,000 rpm
Repeat positioning accuracy
±0.02 mm
Machine weight
Approx. 1,600 kg
Process
CNC machining
Specifications support preliminary selection. Capacity varies with profile geometry, cutting angle, tooling and clamping. Values marked “to be confirmed” are not published in the source data. Confirm the supplied configuration in your quotation.
List the cutters, tool holders, clamp layout and machining faces. Confirm the control/software package and the required drawing or program formats.
Supply and site requirements
State voltage, phase and frequency, control requirements and destination. Ask the quotation to distinguish included equipment, options, packing, documentation and installation or training arrangements.
What to include with your drawing
Profile section, material and stock length
Finished-part drawing, angles and critical dimensions
Production quantity and current process
Electrical supply, tooling and workshop requirements
For a machine review, include the sample operation, critical feature and finish you want to check. Ask CAMAS for model-specific footage or sample details when requesting your configuration.
What does three-face machining mean for this configuration?
The table presents the profile at the published positions. Review whether the actual features, tools and clamps permit the planned faces to be machined in that setup; it does not establish access to every possible feature.
How do I know this configuration fits my part?
Send the finished-part drawing, material, dimensions and quantity. Review tooling access, working capacity and handling together before selecting the configuration.
What tools are included?
The agreed quotation defines the supplied blades, dies, cutters, gauges and accessories. Include your required holes, angles and features so the tool package can be itemized.
Can I specify the electrical supply?
Include voltage, phase and frequency in your inquiry. Electrical variations and control requirements should be confirmed for the specific configuration.
How are delivery and support arranged?
Delivery timing, packing, installation, training and spare-parts scope are agreed for the project. Share the destination and your site requirements when requesting a quotation.